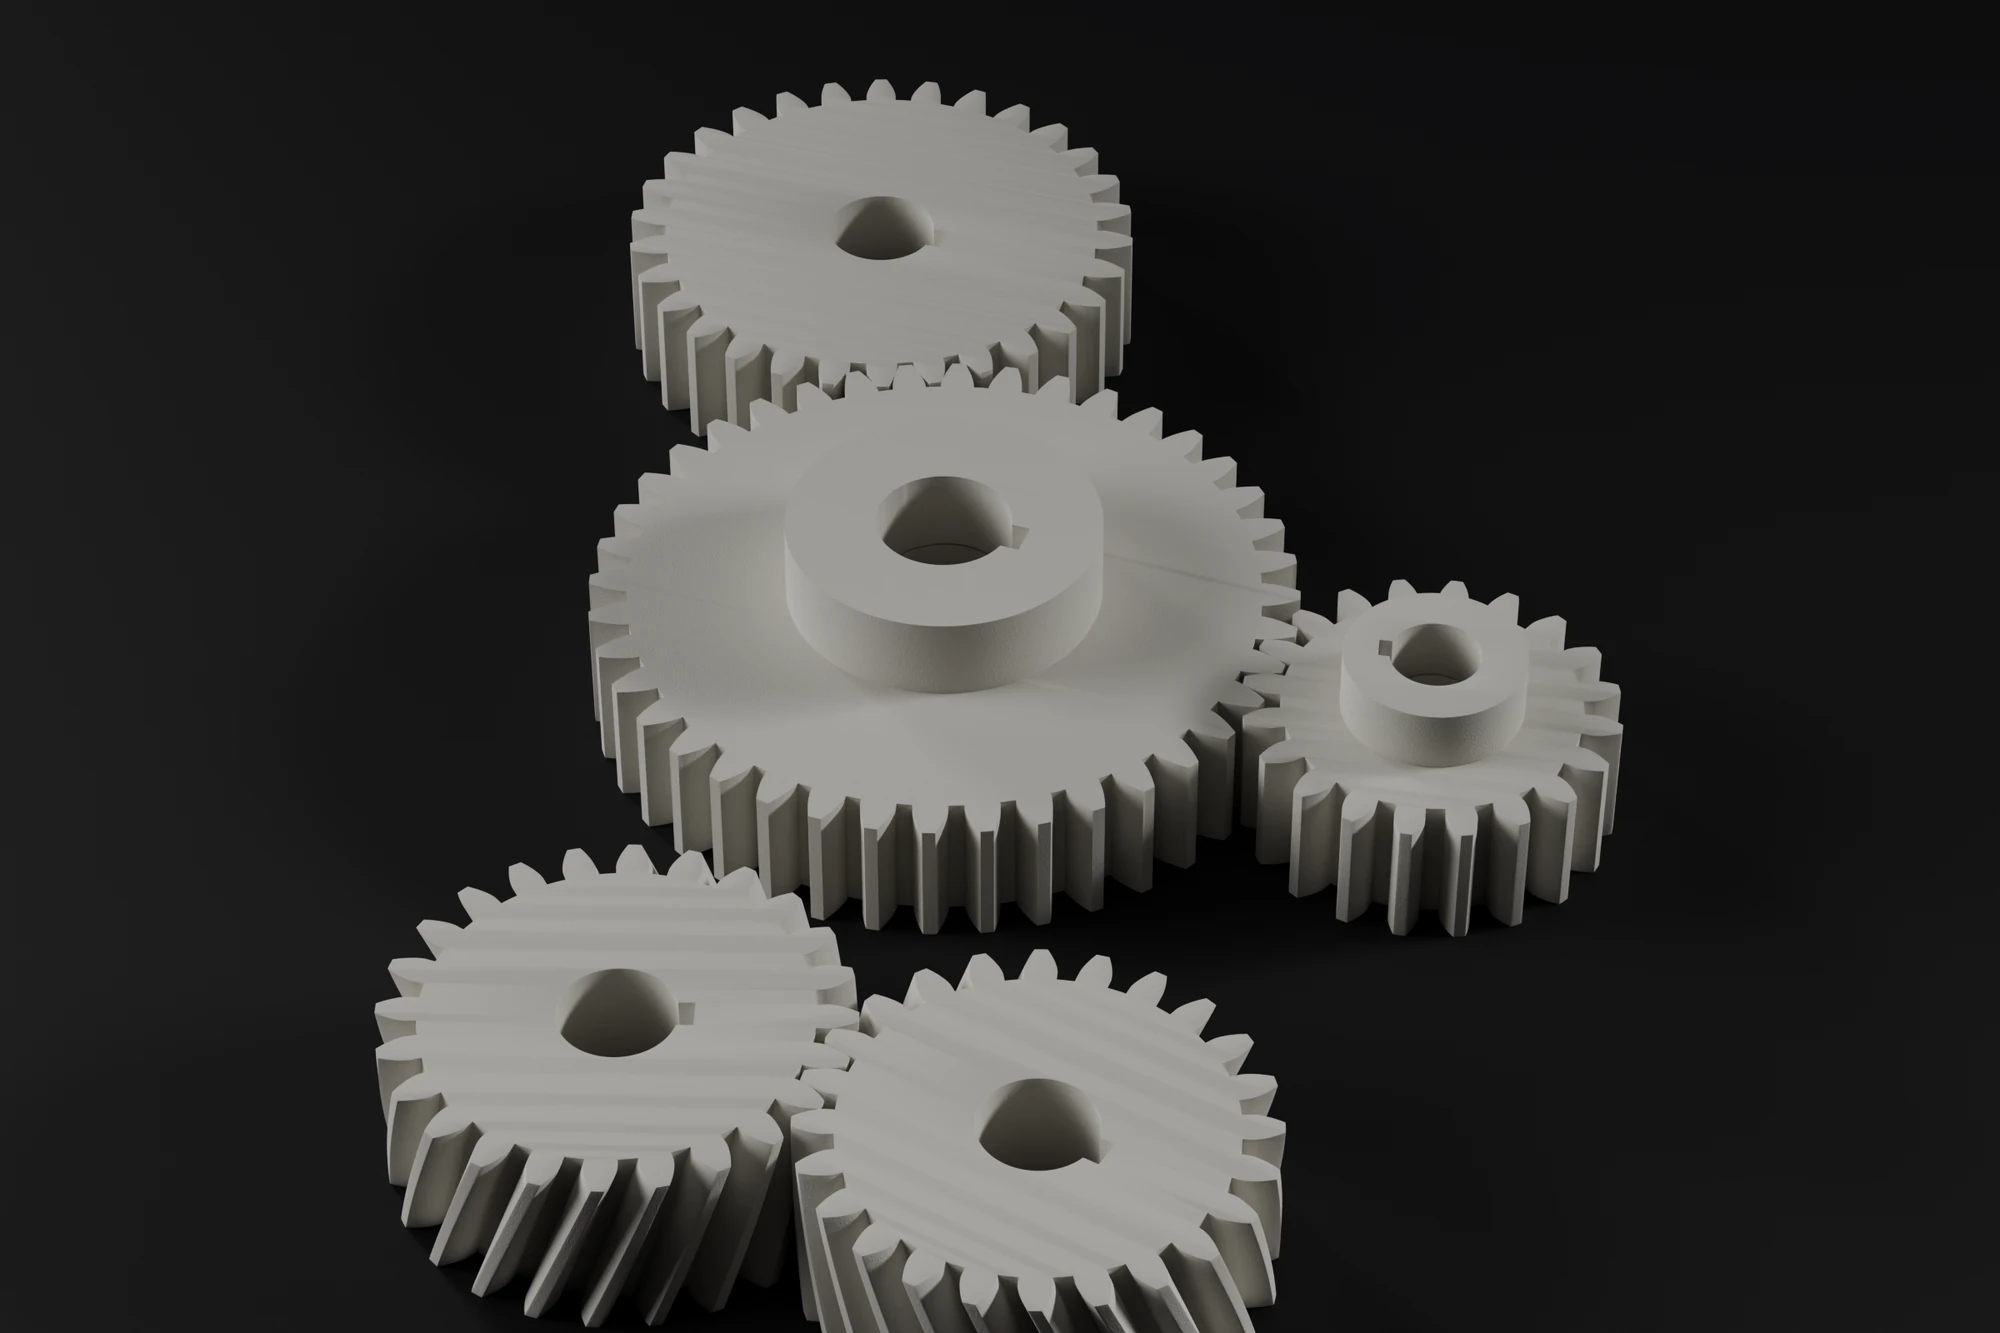
What is PA12 nylon?
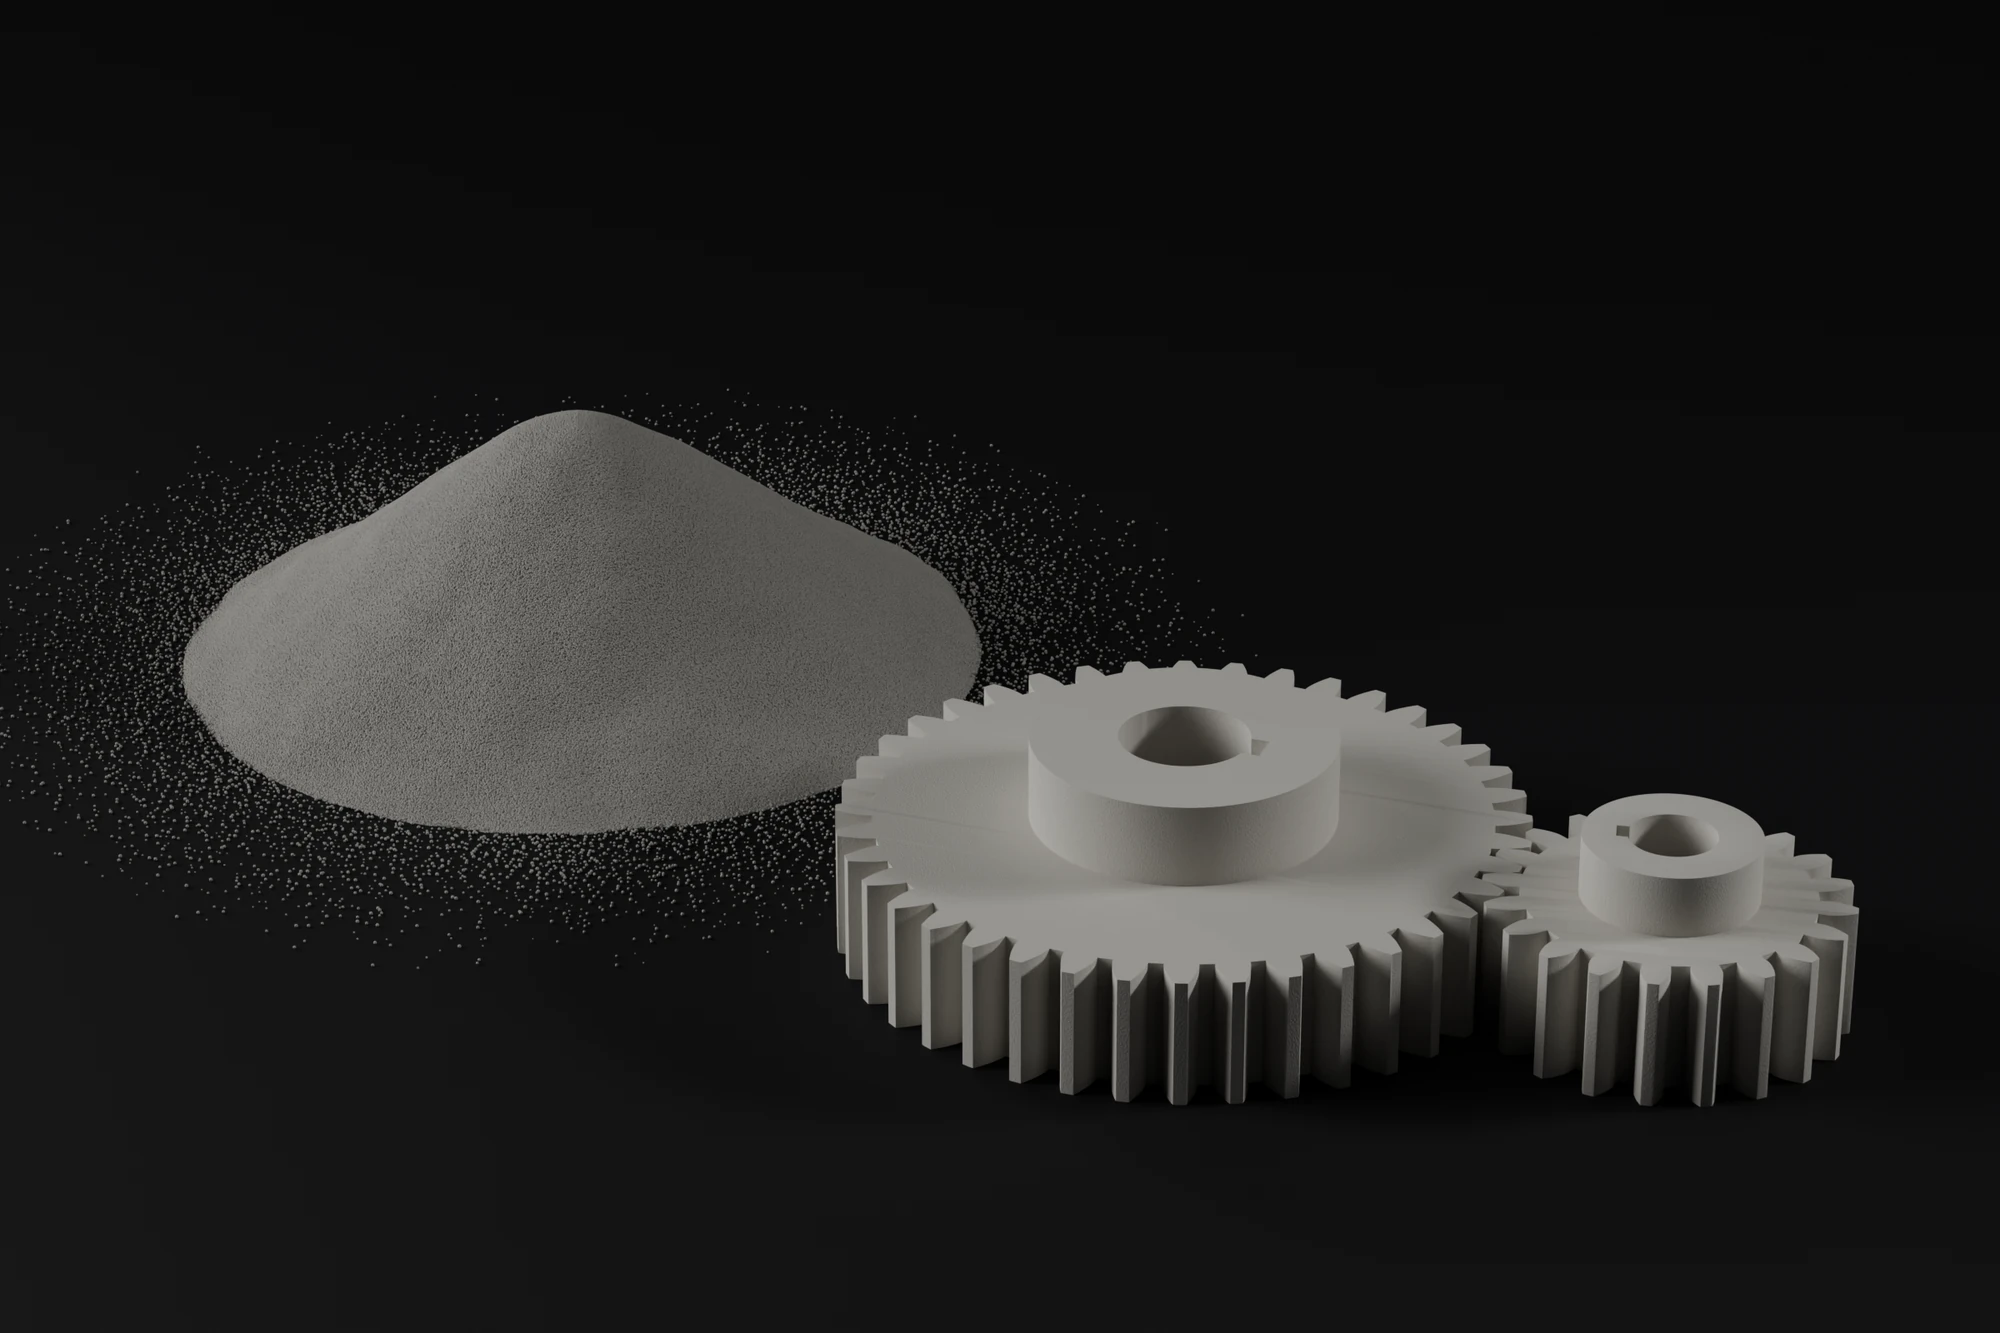
PA12 is polyamide 12, a nylon. It is one of the powders we print in SLS, and the one our SLS design rules are written for. A laser fuses the powder layer by layer, and the loose powder holds the part while it prints.
Nylon is strong and slightly flexible, with good fatigue resistance and low friction. That is why engineers reach for it when a part has to move, wear or flex many times.
PA12 takes up less moisture than many other nylons, so it stays more dimensionally stable. Printed nylon parts still take up some moisture from the air.
Where PA12 performs: gears, hinges, clips, housings
- Gears and plain bearings. Low friction and good wear behaviour.
- Hinges and living hinges. Fatigue resistance for repeated bending.
- Clips and snap fits. Slightly flexible, so they bend before they break.
- Housings, ducts and connectors. Strong, with no support marks.
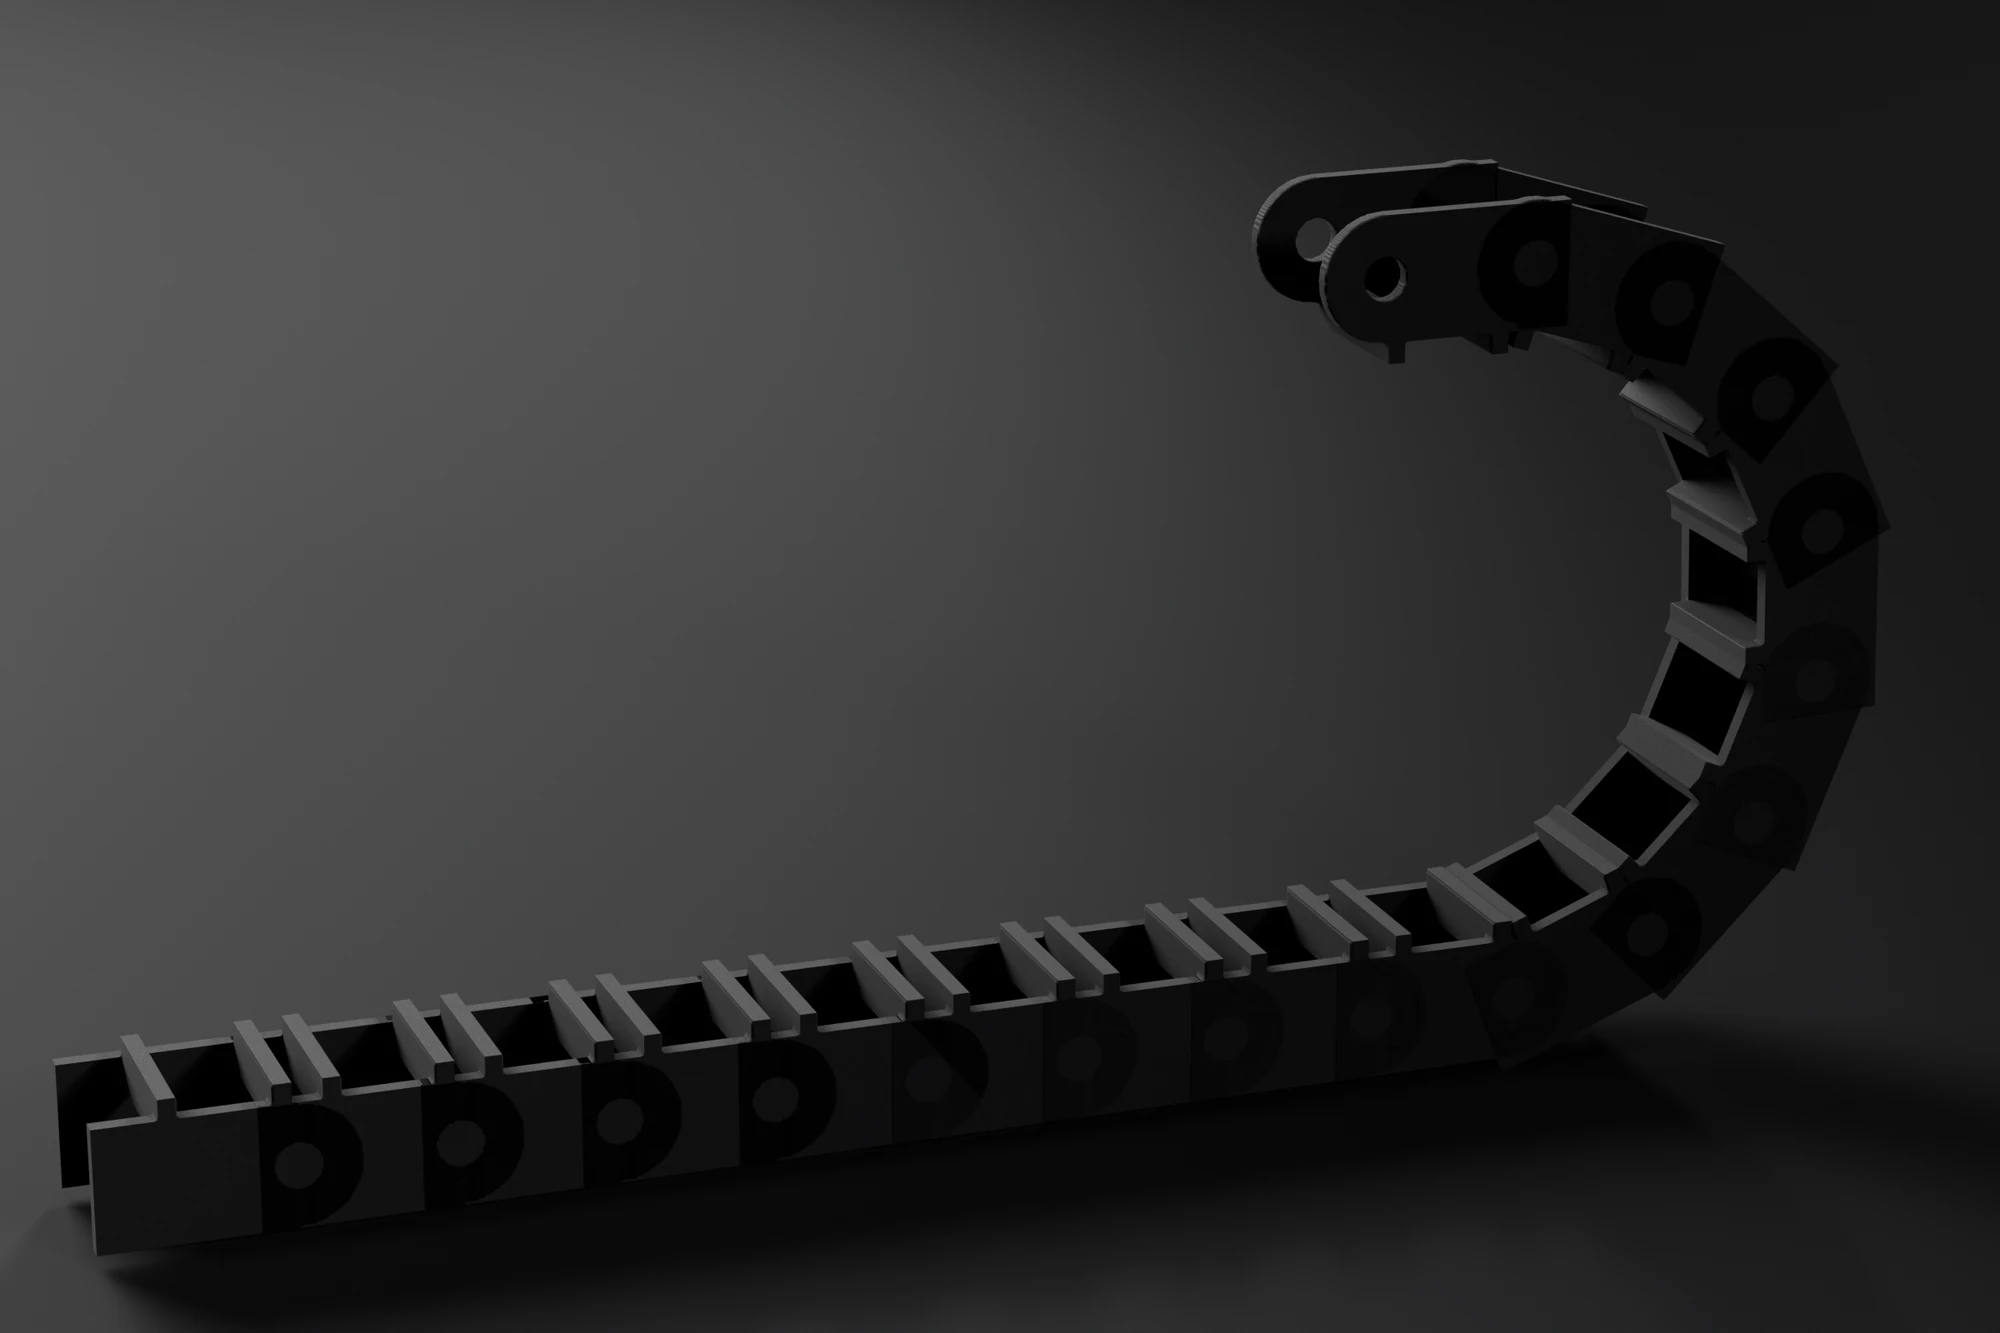
- Moving assemblies. Chains and linked parts can come out of the powder already assembled.
Typical uses also include functional prototypes, jigs and small series. See jigs and fixtures.
PA12 in SLS: why the process fits the material
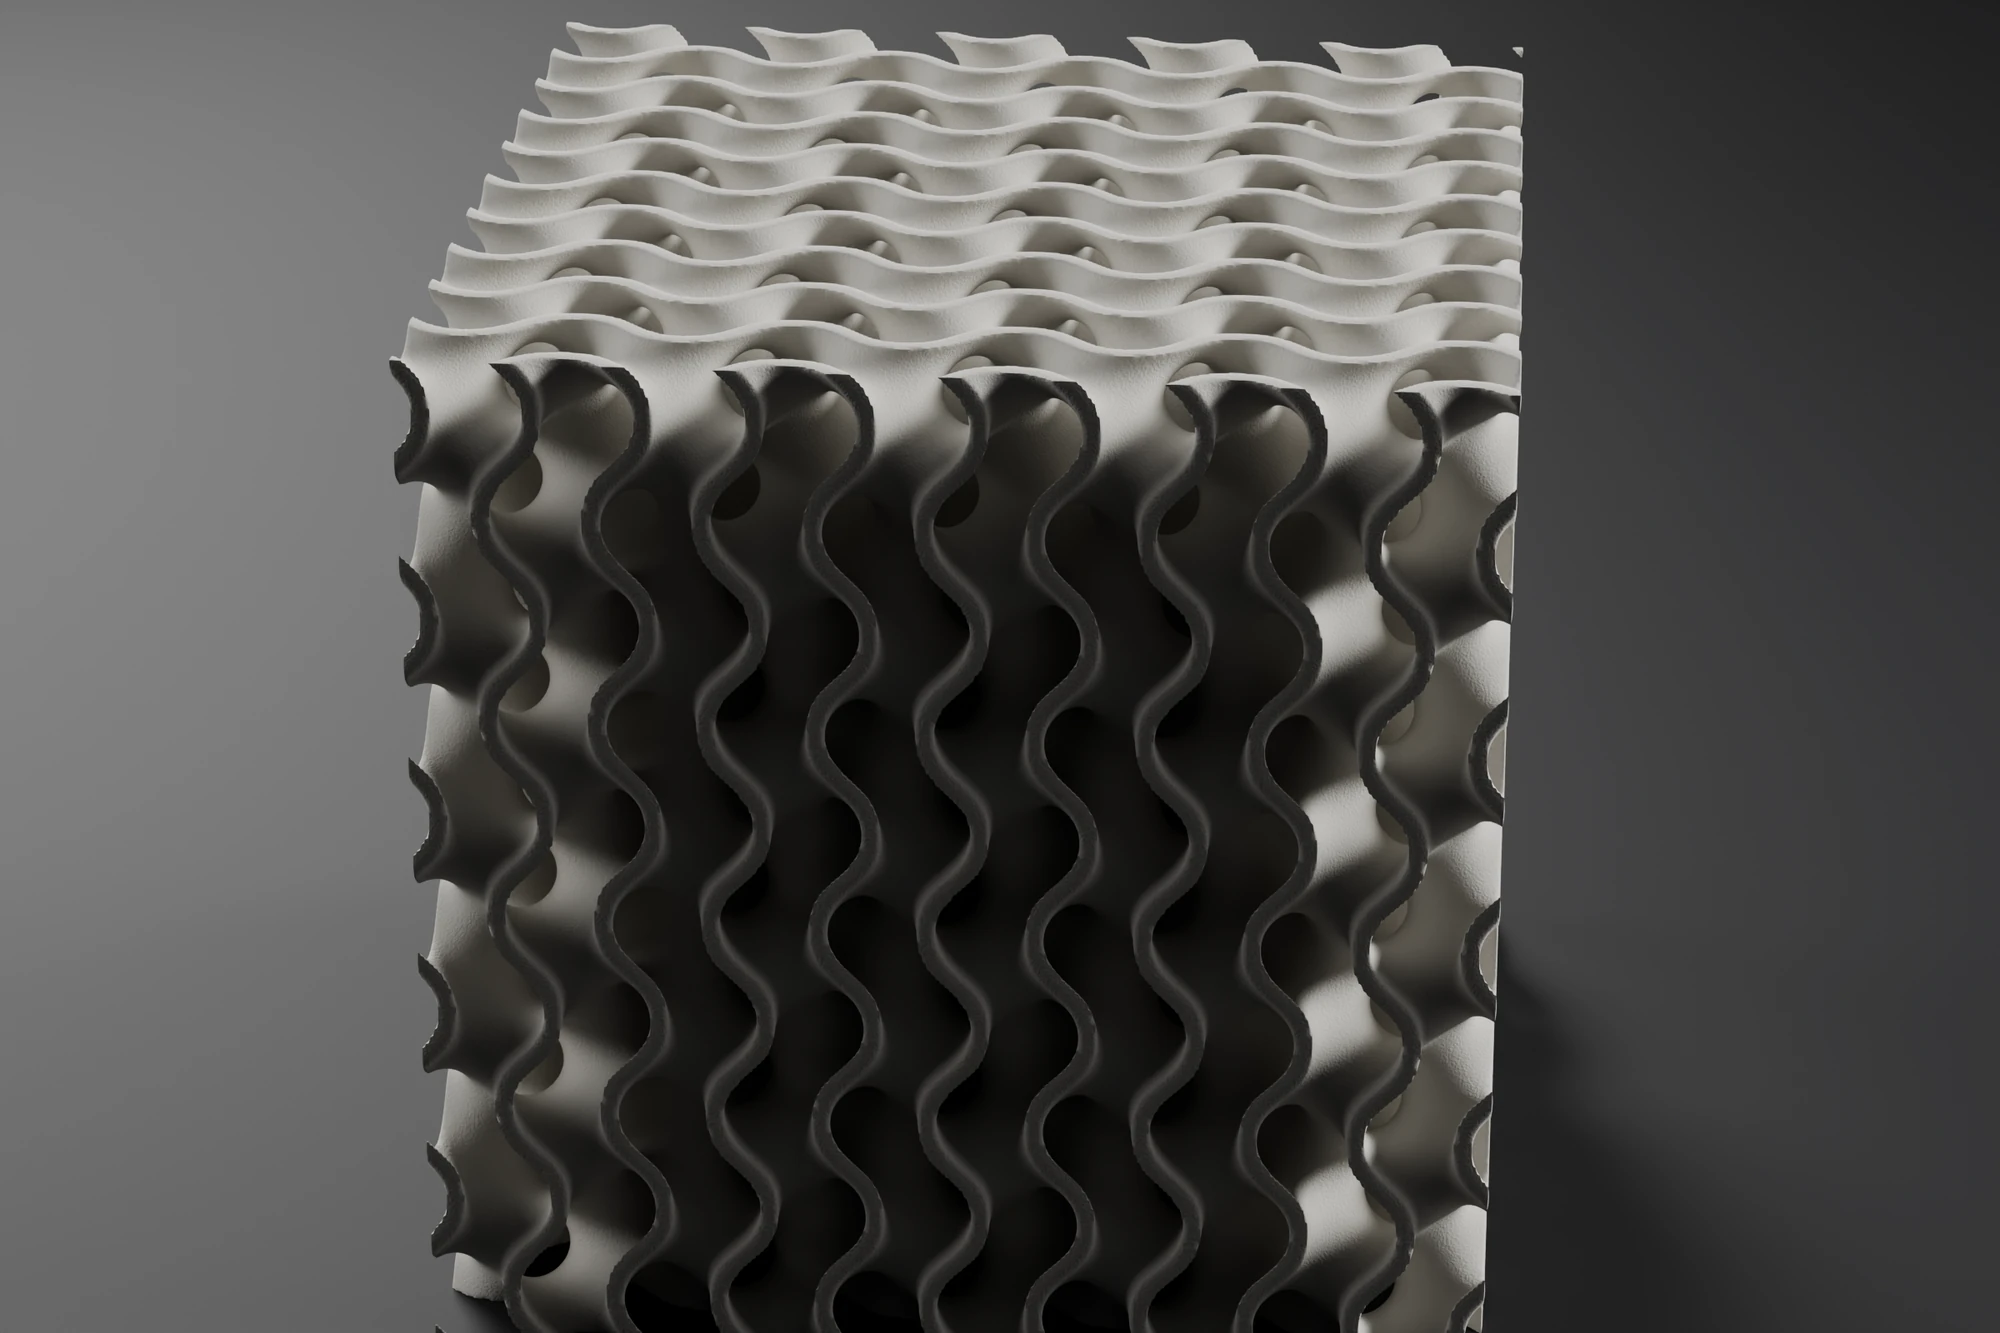
In SLS the powder supports the part, so overhangs, internal channels and lattices need no supports. Parts are nearly equally strong in every direction, much more so than FDM parts, which are weakest between layers. Parts can be nested through the whole build volume, which suits series and spare parts.
FDM nylon is a different story: it absorbs moisture from the air, so the filament must be dried before printing and stored sealed. For high stress or wear, SLS is our pick.
Read the SLS page for the process.
PA12 compared with PA-CF and PA-GF
PA-CF (carbon-filled) and PA-GF (glass-filled) are filled powders. Filled grades are typically stiffer, but more brittle, with a rougher surface. They have their own limits, so ask us before you design for them. All design values on this page are for PA12.
Design rules for PA12 parts
| Feature | Rule |
|---|---|
| Wall thickness | 1.0 mm or more. 2.0 mm or more if the wall carries load. |
| Holes | 1.5 mm diameter or more |
| Raised or engraved text | 1.0 mm high or deep or more |
| Moving gaps | 0.5 mm or more, 1.0 mm on larger contact areas |
| Hollow parts | At least two powder drain holes of 5 mm or more, at opposite ends. Shell 2.0 mm or more. |
Keep wall thickness even and round inside corners. Put drain holes where powder can fall out, not in a dead-end pocket. If a fit is tight, print the mating parts as a test first. More in the SLS design guide.
Surface and accuracy
PA12 parts are matte with a fine, slightly grainy texture. They are not glossy. Accuracy is typically about ±0.3 mm on smaller parts, and larger parts vary a little more. Leave room where parts must fit together.
Ordering PA12 parts: price, lead time, shipping
We price by the weight of the finished part, with a setup fee once per technology and a handling fee per part. Failed prints are on us. The per-kg rate is on the pricing page. Standard orders ship in 3 to 5 business days, rush in 2. Pickup in Amsterdam is free. We ship with PostNL.